
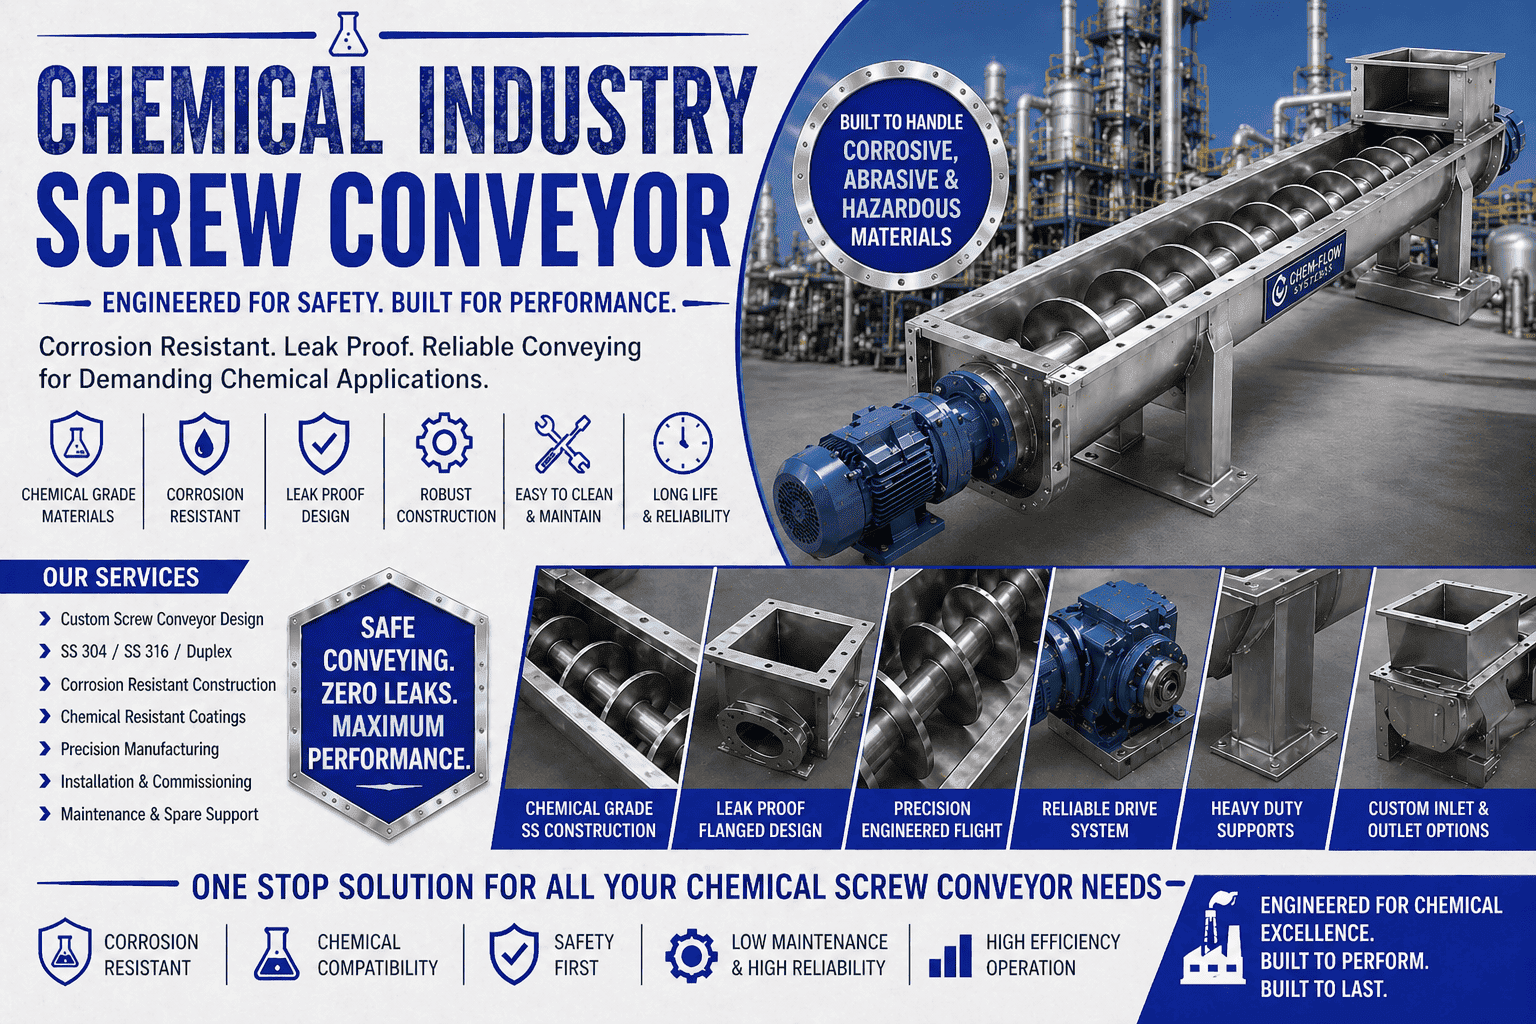
Chemical Industry Screw Conveyor
Virkrupa Engineers is a leading manufacturer and supplier of Chemical Industry Screw Conveyors, delivering precision-engineered, heavy-duty, and corrosion-resistant material handling solutions for chemical processing plants, powder handling units, fertilizer industries, bulk material systems, and industrial manufacturing sectors. Designed with advanced fabrication technology, robust engineering, and industry-focused safety standards, our screw conveyors ensure efficient, secure, and controlled transportation of chemical powders, granules, and industrial raw materials.
From chemical powders and minerals to fertilizers, additives, and bulk industrial compounds, Virkrupa Engineers provides customized screw conveyor systems that improve operational efficiency, reduce material loss, and support safe industrial processing.
Chemical Industry Screw Conveyor is designed for the safe and efficient conveying of powders, granules, chemicals, and other bulk materials in chemical processing plants. Manufactured from high-quality stainless steel and other suitable materials, these conveyors provide excellent corrosion resistance, durability, and reliable performance in demanding industrial environments. Enclosed screw conveyor systems help minimize dust, material spillage, and contamination during transportation. They are suitable for horizontal, inclined, and customized material handling applications. Chemical screw conveyors can be designed according to required capacity, conveyor length, material characteristics, and process requirements. Their robust construction, smooth operation, and low maintenance make them an effective solution for continuous chemical material handling and powder transfer applications.
Chemical Screw Conveyor
A Chemical Screw Conveyor is an efficient material handling system designed for the safe and continuous conveying of chemical powders, granules, crystals, and other bulk materials. It provides controlled movement of materials within chemical processing plants, production facilities, and industrial applications. Manufactured using durable materials such as stainless steel and mild steel, these conveyors can be customized according to material characteristics, capacity, temperature, and conveying distance. Chemical Screw Conveyors offer reliable, low-maintenance operation and consistent material flow. They are suitable for horizontal, inclined, and customized conveying applications. Their robust construction and enclosed design help minimize material loss, dust, and contamination during chemical material handling processes.
Screw Conveyor for Chemical Industry
A Screw Conveyor for Chemical Industry is designed for the efficient and controlled handling of chemical powders, granules, crystals, and other bulk materials. It provides smooth and continuous material transportation across chemical processing plants, manufacturing units, and storage facilities. These conveyors are manufactured using durable Mild Steel and Stainless Steel materials, with options for corrosion-resistant construction based on application requirements. Screw conveyors can be customized for different capacities, conveying distances, temperatures, and material characteristics. Their enclosed design helps reduce dust, spillage, and material contamination while ensuring reliable operation. They are suitable for horizontal, inclined, and specialized chemical material handling applications.
Chemical Processing Screw Conveyor
A Chemical Processing Screw Conveyor is an efficient industrial conveying system designed to transport chemical powders, granules, crystals, and other bulk materials during processing operations. It provides controlled, continuous, and reliable material movement between different stages of chemical production. Manufactured from Mild Steel or Stainless Steel, these conveyors can be customized with corrosion-resistant materials and components according to specific chemical handling requirements. Chemical Processing Screw Conveyors are suitable for horizontal, inclined, feeding, dosing, and discharge applications. Their enclosed construction helps minimize dust, spillage, and contamination while maintaining consistent material flow. They are widely used in chemical plants, processing units, manufacturing facilities, and bulk material handling systems.
Chemical Material Handling Conveyor
A Chemical Material Handling Conveyor is designed for the safe, efficient, and continuous transportation of chemical powders, granules, crystals, and bulk materials in industrial facilities. It helps move materials between processing, storage, mixing, feeding, and packaging areas with controlled and consistent flow. These conveyors can be manufactured from Mild Steel or Stainless Steel, with suitable corrosion-resistant components for demanding chemical applications. Chemical Material Handling Conveyors are available in horizontal, inclined, and customized configurations to meet different capacity and layout requirements. Their enclosed conveying design helps reduce dust, spillage, and contamination. They are widely used in chemical plants, processing units, and industrial material handling applications.
Chemical Powder Screw Conveyor
A Chemical Powder Screw Conveyor is an efficient material handling solution designed for the controlled transportation of chemical powders and fine bulk materials. It provides smooth, continuous movement of materials between processing, storage, mixing, feeding, and packaging systems. These conveyors can be manufactured from Mild Steel or Stainless Steel with suitable corrosion-resistant construction for specific chemical applications. The enclosed design helps minimize dust, spillage, and material contamination while maintaining consistent material flow. Chemical Powder Screw Conveyors can be customized according to conveying capacity, material properties, distance, inclination, and operating conditions. They are widely used in chemical plants, processing units, and industrial bulk material handling applications.
Chemical Granules Screw Conveyor
A Chemical Granules Screw Conveyor is designed for the efficient and controlled transportation of chemical granules and other bulk materials in industrial processing applications. It provides smooth and continuous material movement between storage, processing, mixing, feeding, and packaging equipment. These conveyors can be manufactured from Mild Steel or Stainless Steel with corrosion-resistant components according to the chemical properties of the material. The enclosed conveying system helps minimize dust, spillage, and material contamination while maintaining consistent flow. Chemical Granules Screw Conveyors can be customized based on capacity, conveying distance, material characteristics, temperature, and installation requirements. They are suitable for chemical plants, processing units, and bulk material handling systems.
Chemical Resistant Screw Conveyor
A Chemical Resistant Screw Conveyor is designed for the safe and reliable transportation of corrosive chemicals, powders, granules, crystals, and other bulk materials. It is manufactured with corrosion-resistant materials and components selected according to the chemical properties and operating conditions of the application. Stainless Steel construction and suitable protective finishes can provide enhanced durability in demanding chemical environments. The enclosed conveyor design helps minimize dust, spillage, and material contamination while ensuring smooth and continuous material flow. Chemical Resistant Screw Conveyors can be customized for different capacities, conveying distances, temperatures, and installation layouts. They are suitable for chemical plants, processing units, and industrial bulk material handling applications.
Dry Chemical Handling Conveyor
A Dry Chemical Handling Conveyor is designed for the efficient and controlled transportation of dry chemical powders, granules, crystals, and other bulk materials. It provides continuous material movement between storage, processing, mixing, feeding, and packaging equipment in chemical manufacturing facilities. These conveyors can be manufactured using Mild Steel or Stainless Steel, with corrosion-resistant construction selected according to the material and operating environment. The enclosed conveying system helps minimize dust, spillage, and contamination while maintaining a consistent material flow. Dry Chemical Handling Conveyors can be customized for different capacities, conveying distances, temperatures, and installation layouts, making them suitable for chemical plants and industrial material handling applications.
Chemical Powder Handling Equipment
Chemical Powder Handling Equipment is designed for the safe, efficient, and controlled handling of chemical powders and other dry bulk materials in industrial processing facilities. It helps transfer, feed, convey, store, and discharge powdered materials with consistent flow and reduced material loss. Equipment can be manufactured from Mild Steel or Stainless Steel, with corrosion-resistant construction selected according to specific chemical properties and operating conditions. Enclosed handling systems help minimize dust, spillage, and contamination during material movement. Chemical Powder Handling Equipment can be customized according to material characteristics, capacity, conveying distance, temperature, and plant layout. It is suitable for chemical plants, manufacturing units, processing facilities, and bulk material handling applications.
Chemical Material Handling Equipment
Chemical Material Handling Equipment is designed for the safe, efficient, and controlled movement of chemical powders, granules, crystals, and other bulk materials in industrial facilities. It supports various material handling operations, including conveying, feeding, transferring, loading, and discharge. Equipment can be manufactured from Mild Steel or Stainless Steel, with corrosion-resistant materials and components selected according to application requirements. Enclosed handling systems help minimize dust, spillage, and material contamination while maintaining consistent material flow. Chemical Material Handling Equipment can be customized according to material properties, capacity, conveying distance, temperature, and plant layout. It is widely used in chemical plants, processing units, manufacturing facilities, and bulk material handling systems.
Chemical Plant Conveyor
A Chemical Plant Conveyor is an industrial material handling system designed for the safe and efficient transportation of chemical powders, granules, crystals, and other bulk materials. It provides continuous and controlled material movement between storage, processing, mixing, feeding, and packaging areas within chemical plants. Chemical Plant Conveyors can be manufactured using Mild Steel or Stainless Steel, with corrosion-resistant components selected according to the material and operating conditions. Their enclosed design helps reduce dust, spillage, and contamination during conveying. These conveyors can be customized for different capacities, conveying distances, temperatures, inclinations, and plant layouts. They are suitable for chemical processing plants, manufacturing units, and bulk material handling applications.
Chemical Processing Equipment
Chemical Processing Equipment is designed to support efficient, reliable, and controlled operations in chemical manufacturing and processing plants. It can include equipment for material handling, mixing, blending, conveying, storage, feeding, filtration, separation, and processing of various chemical materials. Depending on the application, equipment can be manufactured using Mild Steel, Stainless Steel, and other suitable materials to provide durability and resistance to demanding operating conditions. Chemical Processing Equipment can be customized according to material characteristics, production capacity, temperature, pressure, and plant requirements. Properly designed systems help improve process efficiency, material handling, operational safety, and consistent production. They are suitable for chemical plants, manufacturing facilities, and industrial processing applications.
Screw Feeder for Chemical Industry
A Screw Feeder for Chemical Industry is designed for accurate, controlled, and continuous feeding of chemical powders, granules, crystals, and other bulk materials into processing equipment. It helps maintain a consistent material flow during mixing, blending, reaction, conveying, and packaging operations. Screw feeders can be manufactured using Mild Steel or Stainless Steel, with corrosion-resistant materials and components selected according to the chemical properties of the handled material. The feeder can be customized for different capacities, feed rates, material characteristics, temperatures, and installation requirements. Its enclosed construction helps reduce dust, spillage, and contamination. Screw Feeders are suitable for chemical plants, processing units, and industrial material handling systems.
Chemical Powder Feeder
A Chemical Powder Feeder is designed for accurate and controlled feeding of chemical powders, fine materials, and dry bulk products into processing equipment. It provides a consistent material flow for applications such as mixing, blending, dosing, conveying, and production processes. Chemical Powder Feeders can be manufactured from Mild Steel or Stainless Steel, with corrosion-resistant materials and components selected according to the chemical properties of the handled material. The feeding system can be customized for different capacities, feed rates, material characteristics, temperatures, and installation requirements. Its enclosed construction helps reduce dust, spillage, and material contamination. These feeders are suitable for chemical plants, processing units, manufacturing facilities, and bulk material handling systems.
Chemical Conveyor Manufacturer in India
A Chemical Conveyor Manufacturer in India provides reliable material handling solutions for the safe and efficient transportation of chemical powders, granules, crystals, and other bulk materials. Chemical conveyors are designed for continuous and controlled material movement in chemical plants, processing units, manufacturing facilities, and storage systems. Depending on the application, conveyors can be manufactured using Mild Steel, Stainless Steel, and suitable corrosion-resistant materials. They can be customized according to material characteristics, conveying capacity, distance, temperature, inclination, and plant layout. Chemical conveyors help minimize dust, spillage, and material contamination while maintaining consistent material flow. Manufacturers in India offer customized conveyor systems for diverse chemical handling and processing requirements.
Chemical Handling Equipment Manufacturer
A Chemical Handling Equipment Manufacturer provides durable and efficient equipment for the safe handling, conveying, feeding, transferring, and processing of chemical powders, granules, liquids, and other industrial materials. Chemical handling equipment can be manufactured using Mild Steel, Stainless Steel, and suitable corrosion-resistant materials based on specific application requirements. Equipment can be customized according to material properties, capacity, temperature, operating conditions, and plant layout. Well-designed systems help improve material flow, reduce dust and spillage, and support efficient plant operations. Chemical Handling Equipment Manufacturers serve chemical plants, processing units, manufacturing facilities, and bulk material handling industries with customized solutions for reliable and continuous industrial material handling applications.


